ENGINEERING · CASTING · PRECISION MANUFACTURING
OUR MANUFACTURING PROCESS
Engineering precision and quality control at every stage, from design to delivery.
Explore the process1973ISO 484CAD/CAM
MANUFACTURING CAPABILITY
Controlled production from design to sea
Wageningen, Gawn and Kaplan fixed-pitch propellers are engineered for the vessel duty profile using analysis software, AMD and CAD/CAM workflows. Project-specific production complements the standard model families.
EIGHT CONTROLLED STAGES
The manufacturing journey of a propeller
Each stage is planned to secure the geometry and material quality required by the next operation.
-
01
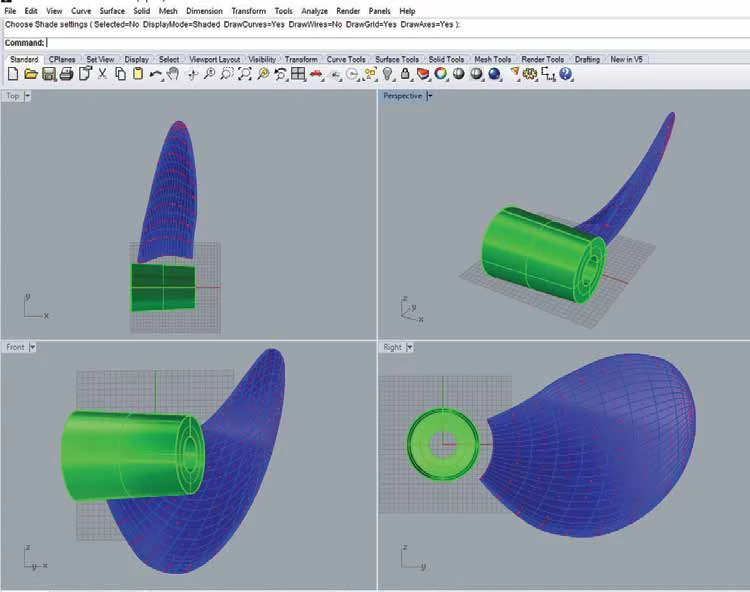
Eriş production archive · 01 Design and propeller selection
Vessel, engine, gearbox and duty profile are assessed together; analysis results are combined with manufacturing experience to create a standard or project-specific geometry.
-
02
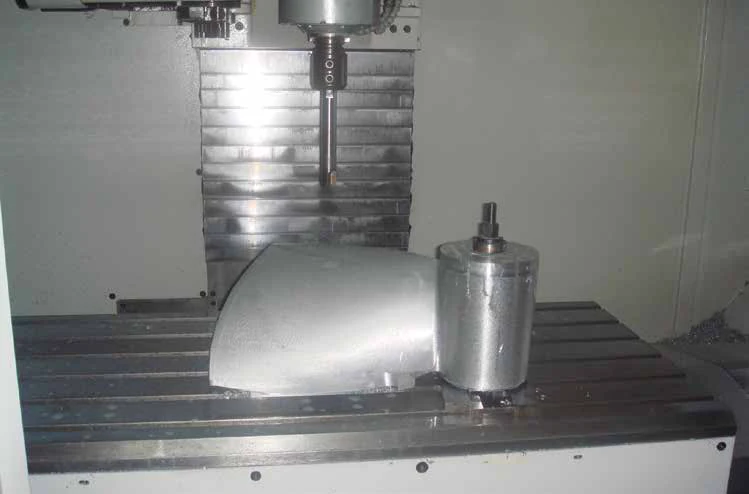
Eriş production archive · 02 Pattern production
AMD and CAD/CAM data are transferred to the production pattern; the blade geometry is prepared on CNC machinery before moulding.
-
03
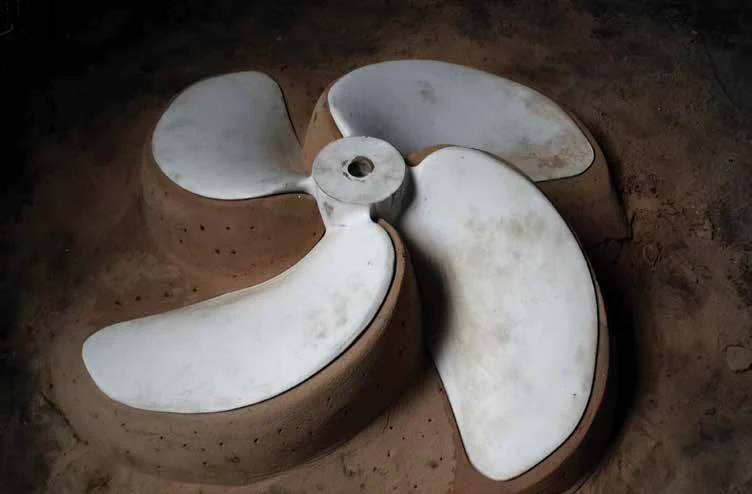
Eriş production archive · 03 Moulding
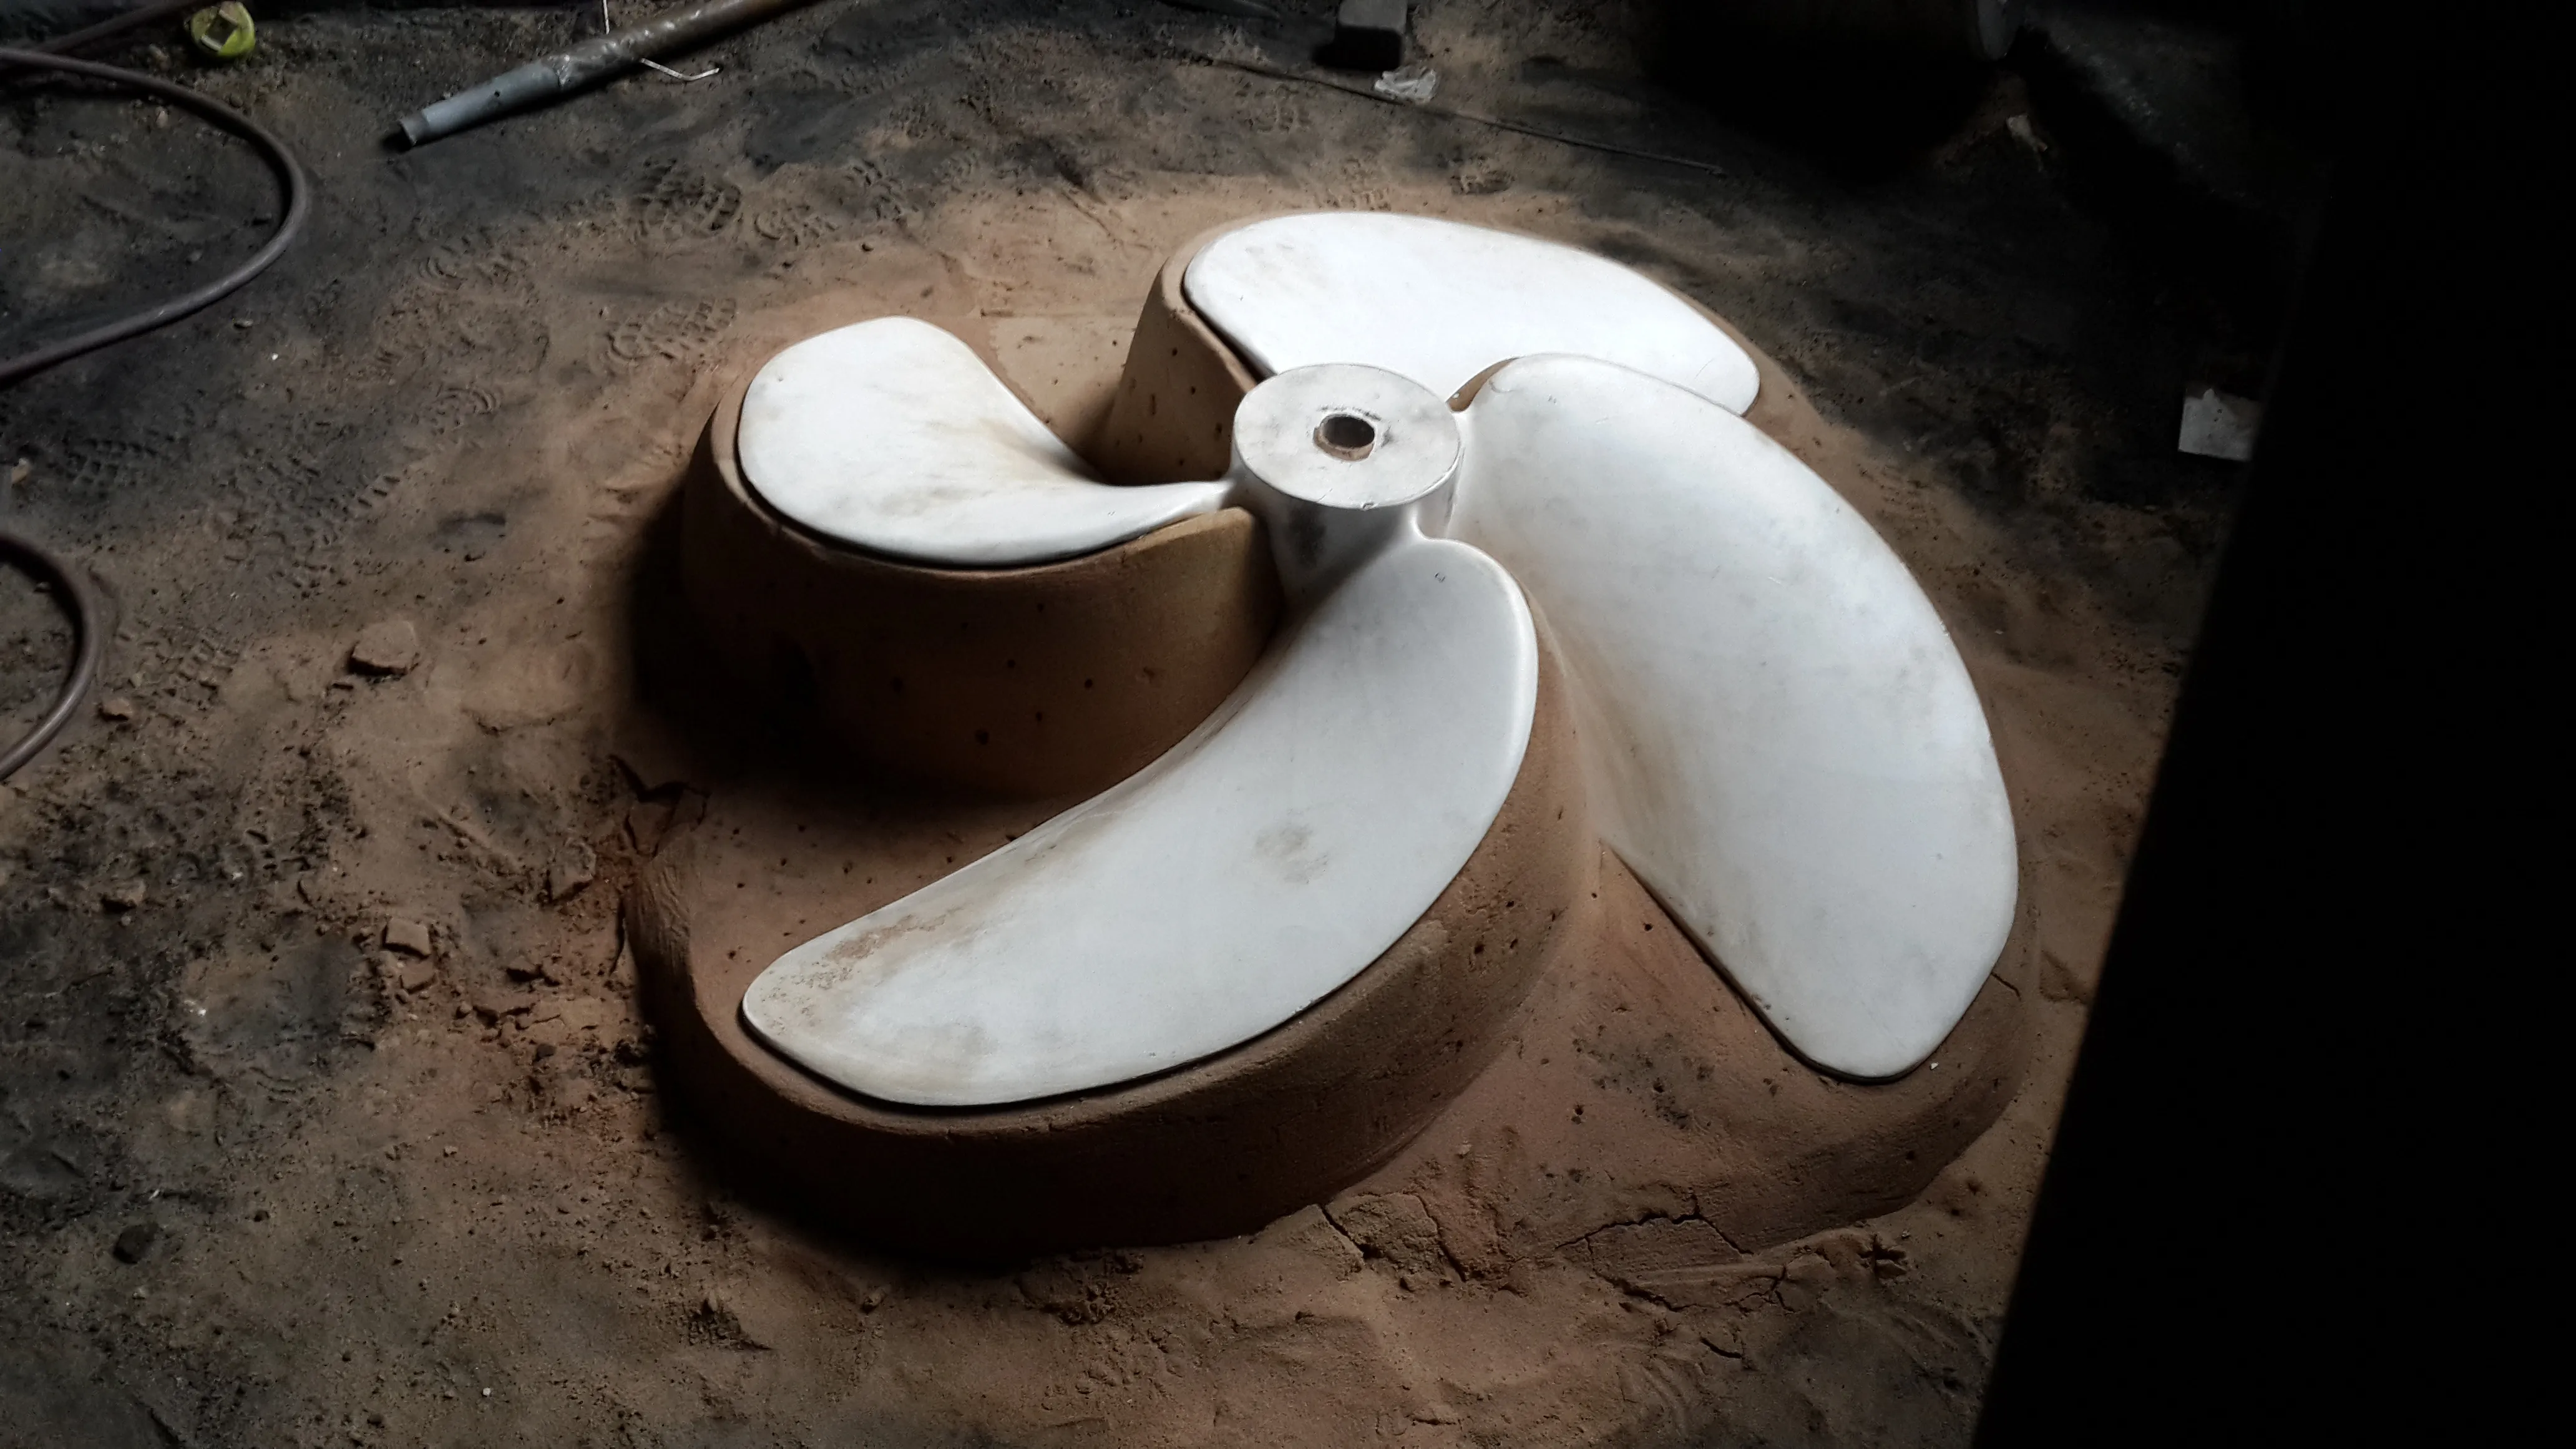
Experienced craftspeople prepare moulds matched to the production pattern for propellers in the 100–2500 mm diameter range.
-
04
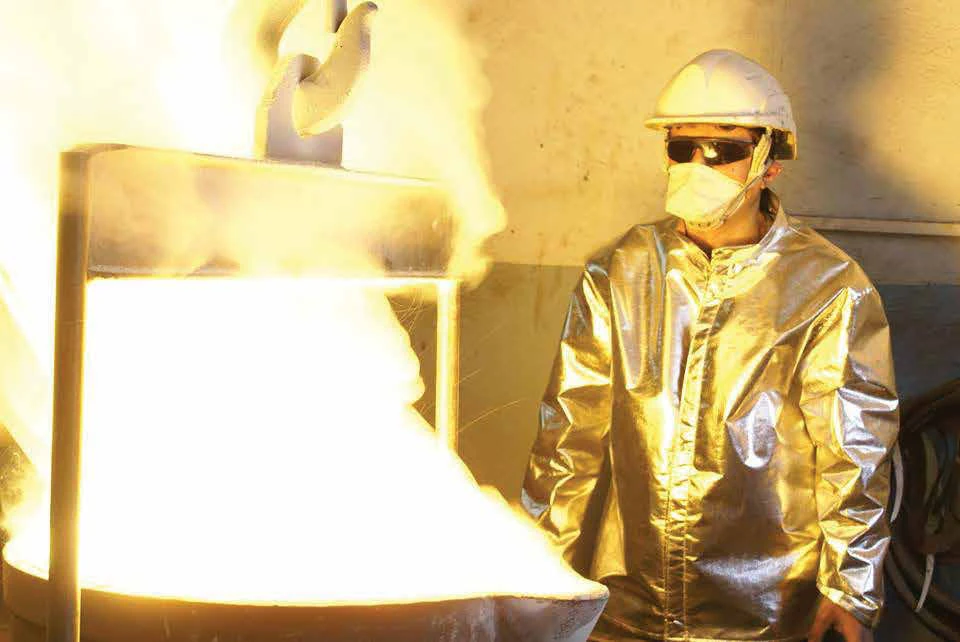
Eriş production archive · 04 Controlled casting
Manganese bronze and nickel-aluminium bronze (Nibral) options are cast under control using electric-furnace infrastructure with up to 2500 kg capacity.
-
05
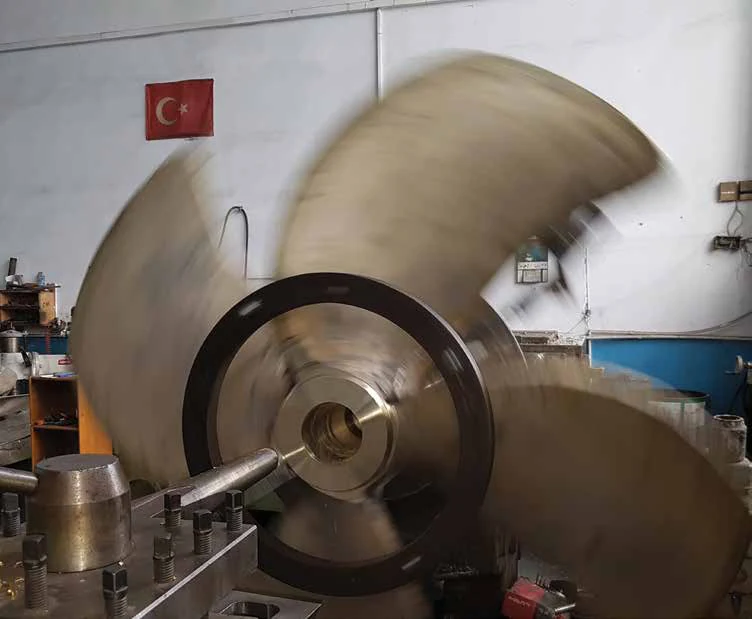
Eriş production archive · 05 Turning and machining
The cast hub and blades are machined on horizontal and vertical equipment to bring connection details and blade geometry to their dimensional targets.
-
06
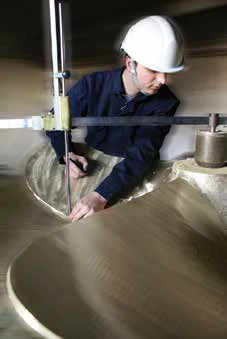
Eriş production archive · 06 Hand finishing and surface refinement
Experienced craftspeople hand-finish the blade surfaces to their final geometry and target surface quality.
-
07
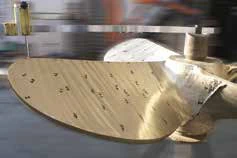
Eriş production archive · 07 Static balancing and final inspection
Dimensions, blade surfaces, material condition and static balance are checked before the final inspection defined by the project scope is completed.
-
08
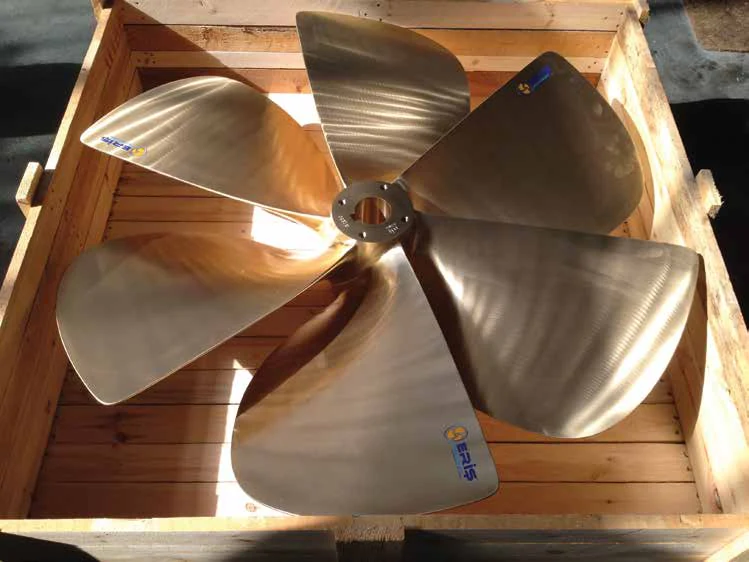
Eriş production archive · 08 Protective packing and dispatch
After final inspection, the blade edges, surfaces and hub connection are secured and wrapped before the propeller is prepared for dispatch in a wooden crate.
ISO · KLAS · MALZEME
Manufacturing to ISO and class tolerances
Standard model cards are specified as ISO 484 Class II. Class supervision, material analysis and certified production options are evaluated according to project requirements.
Technical dimensions and tolerance tablesFOR YOUR PROJECT
Review your project with our manufacturing team
Share your vessel and propulsion data so we can define the model, material, tolerance and delivery scope together.
Contact the manufacturing team